
Industrial Burners for Food Processing Machinery
Our industrial burners are meticulously engineered to meet the high-performance demands of modern food processing applications. Whether for boiling, roasting, frying, or steam generation, these burners ensure consistent heat output, fuel efficiency, and process control, making them the ideal choice for food processing machinery across diverse sectors.
Product Overview:
Our burners are designed to integrate seamlessly with various types of food processing equipment, including:
- Batch and continuous fryer
- Rotary drum roasters
- Deep fryers
- Tilting boiling pans
- Steam jacketed vessels
- Batch and continuous ovens
Available in forced draft burners designs, each unit is built for high thermal output, low maintenance, and safe operation in industrial environments.
Get A Free QuoteKey Features & Benefits
1. High Efficiency Combustion
- Precision flame distribution ensures uniform heat transfer to cooking vessels or heating surfaces.
- Optimized fuel-air mixture design enhances combustion efficiency, reducing fuel consumption and operating costs.
2. Heavy-Duty Construction
- Manufactured from high-grade cast iron, stainless steel, or heat-resistant alloys to ensure durability under continuous operation.
- Corrosion-resistant materials comply with hygiene and food safety standards.
3. Precise Temperature Control
- Optional integration with thermostatic or PLC-based control systems.
- Enables fine-tuning of temperatures for sensitive products such as dairy, confectionery, or sauces.
4. Flexible Fuel Options
- Compatible with Natural Gas (NG) or Liquefied Petroleum Gas (LPG), Diesel, LDO and HSD.
- Adjustable pressure and nozzle configurations to suit regional supply standards.
5. Tailor made solution
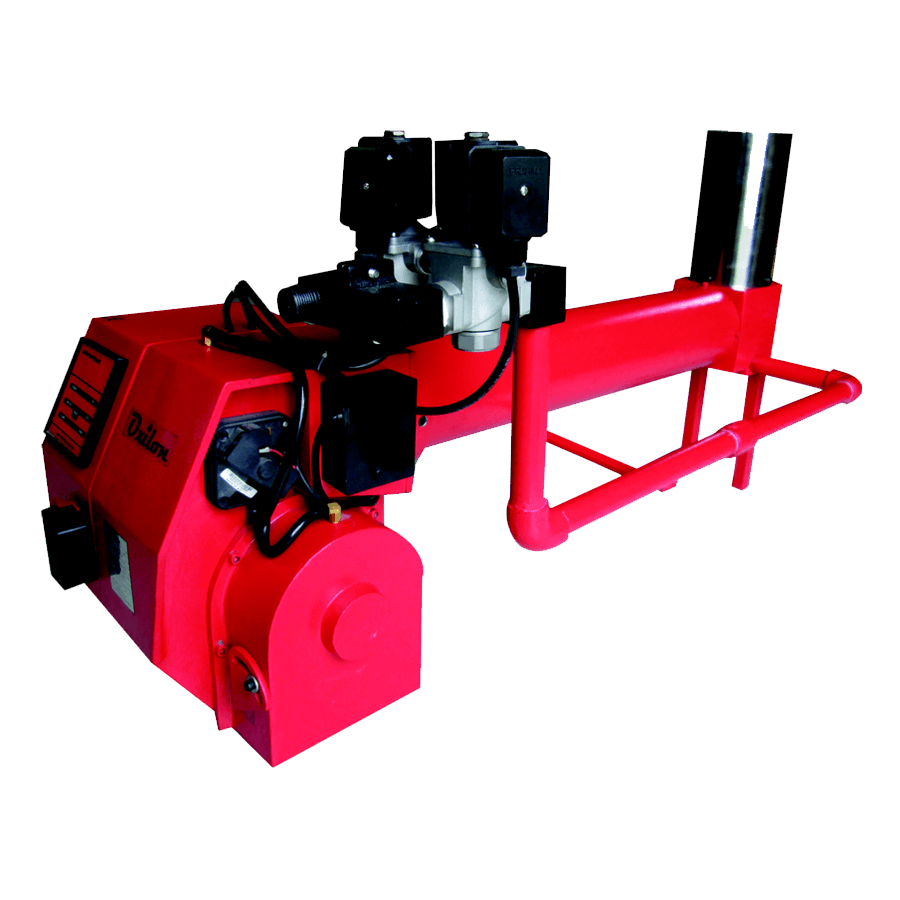
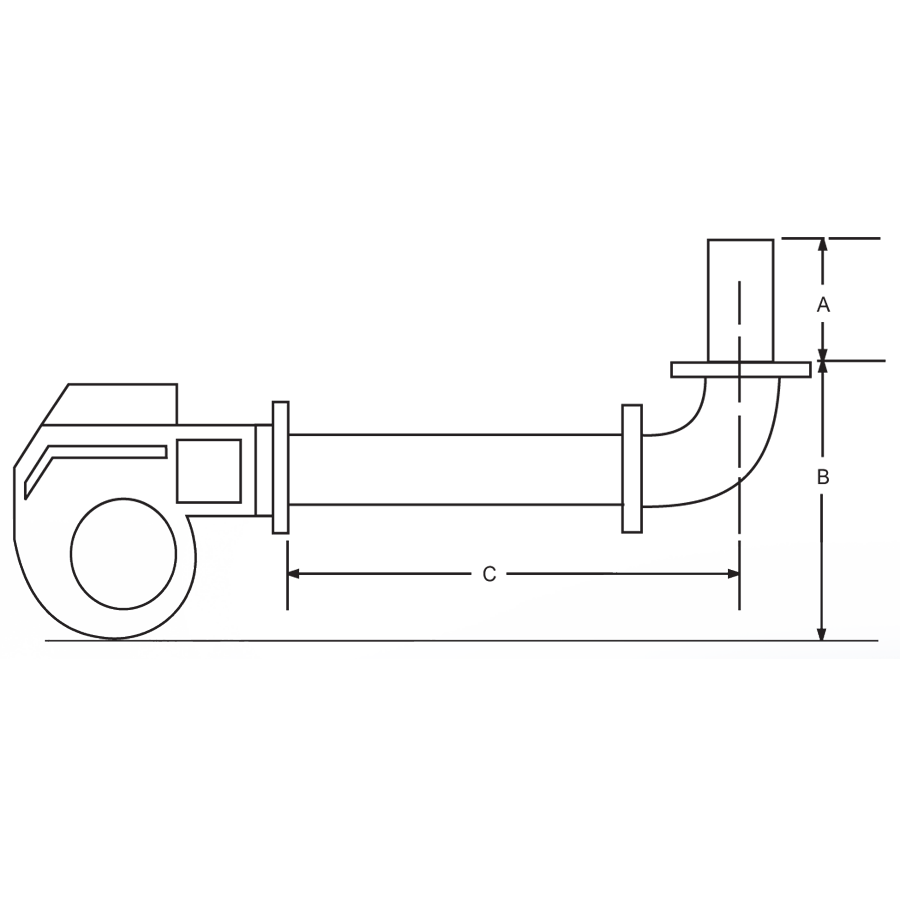
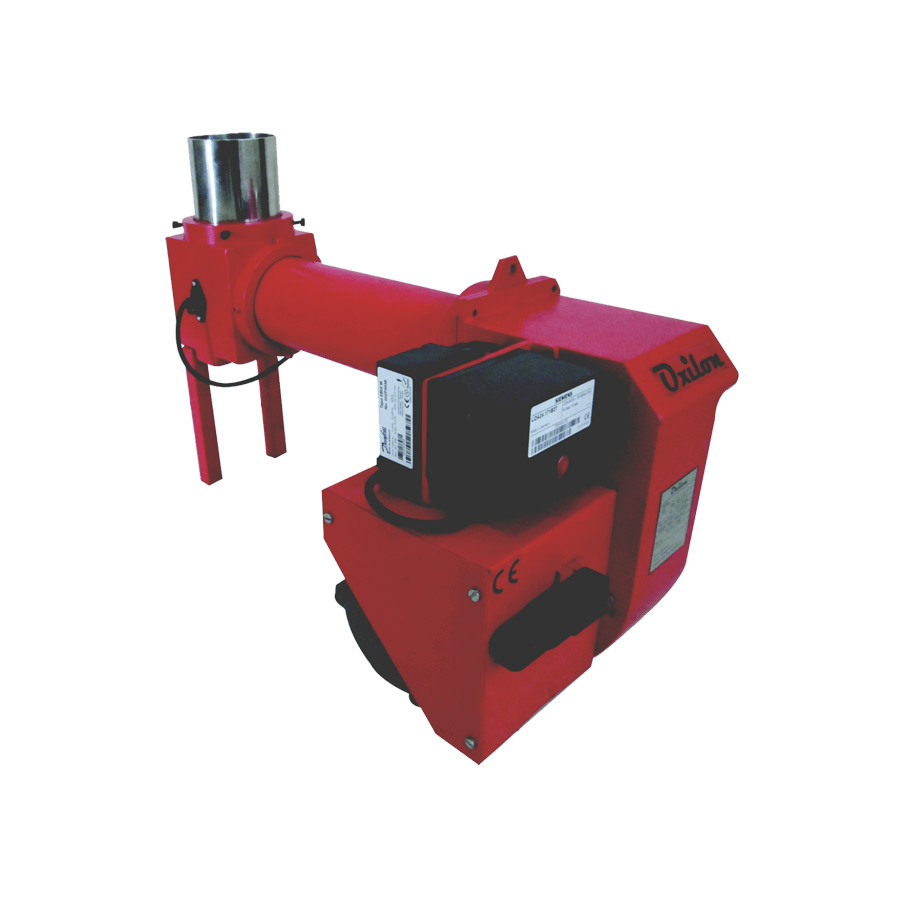
- With the long Bend tube burners for the vertical applications (upward and downward firing).
6. Safety Systems
- Integrated flame failure devices, solenoid valves, and electronic ignition for operator safety and compliance.
- CE/ISO certified models available for export and industrial compliance.
Applications
- Snack Food Manufacturing: Roasting, puffing, frying
- Meat & Poultry Processing: Cooking, boiling, pressure cooking
- Sauces & Curry Production: Controlled boiling and reduction
- Dairy Industry: Milk boiling, ghee processing
- Bakery & Confectionery: Baking, drying, caramelizing
Optional Add-ons & Controls
- Automatic temperature control with PID interface
- PLC/HMI integration for batch or continuous cooking
- Flame monitoring sensors (UV/IR)
- High/low gas pressure regulators for gas burners
- Stainless steel enclosures for wash-down environments
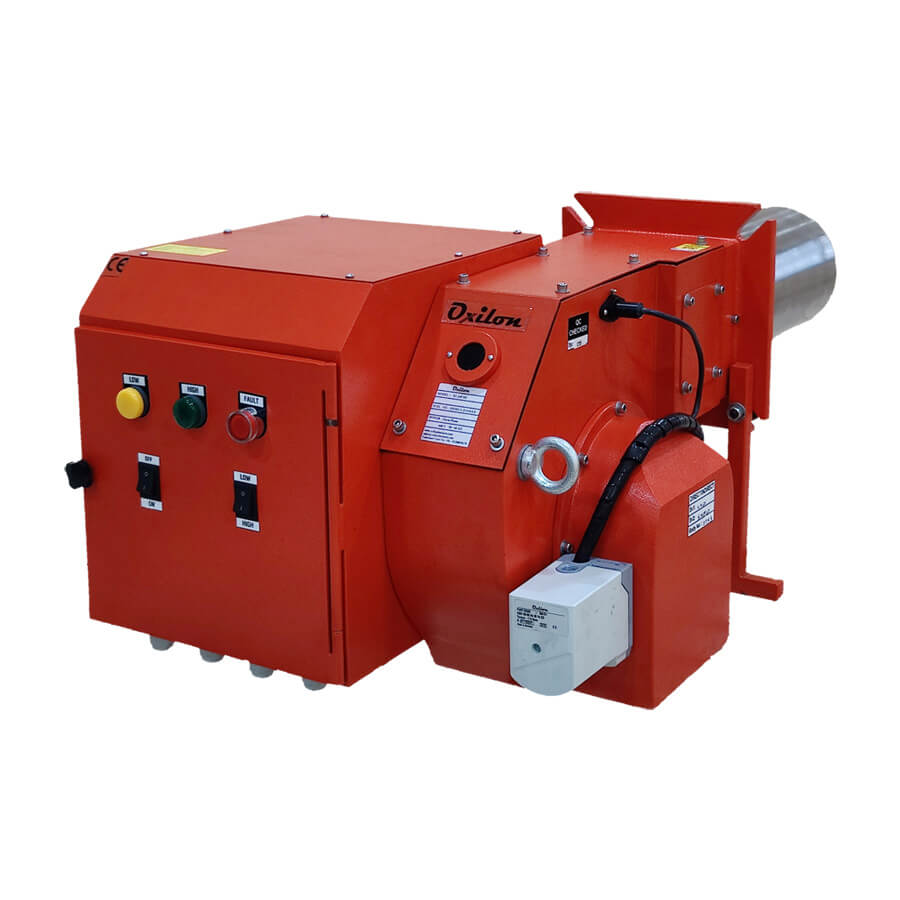
Burner models for Food Processing Machinery

Why Choose Oxilon Burners?
- Engineered for energy efficiency and long operational life
- Designed for easy maintenance and quick installation
- Available in custom configurations based on customer machinery
- Supported by our technical team for integration and troubleshooting


